Related News
 What to Check Before Sourcing a YLCSD350 Cutter Suction Dredger for ProjectsAug 24, 2026
 Battery Cage System of Poultry Farming: What Determines Layer CapacityAug 21, 2026
- China’s Lithium Battery Chain Sees Strong Q2; Overseas Storage Orders LandAug 16, 2026
- China Expands Cross-Border Cash Pooling for Multinationals NationwideAug 15, 2026
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.
Shipbuilding Equipment for Outfitting: What Affects Delivery and Fit-Up Quality





Shipbuilding Equipment for Outfitting: What Affects Delivery and Fit-Up Quality
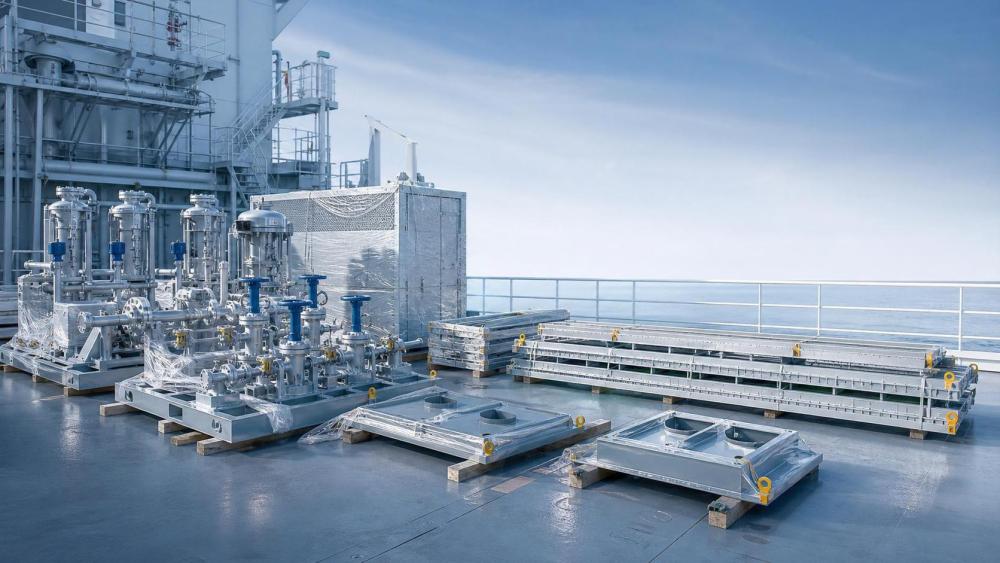
In shipyard projects, shipbuilding equipment for outfitting shapes both schedule certainty and installation quality.
A late valve skid, mismatched support, or inaccurate cable tray can trigger delays across several teams.
That is why delivery performance cannot be separated from fit-up results.
For shipbuilding equipment for outfitting, the biggest risks usually appear at the interfaces.
These include design handover, supplier interpretation, fabrication control, transport protection, and onboard sequencing.
When one interface slips, the knock-on effect often appears during installation, not at purchase order stage.
From recent project patterns, a clearer signal is emerging.
Shipyards that manage outfitting equipment as an integrated flow reduce rework more effectively than those tracking only shipment dates.
The practical question is simple: what actually drives on-time delivery and clean fit-up?
Start With Design Maturity, Not Just Procurement Timing
Many delivery issues begin before fabrication starts.
If drawings are still moving, suppliers may build against frozen dimensions that no longer match block realities.
This is especially common with shipbuilding equipment for outfitting tied to tight spaces.
Think ladders, platforms, pipe supports, HVAC trunks, electrical trays, lockers, and machinery foundations.
If steel structure revisions continue after supplier release, fit-up quality drops fast.
A sound control point is design maturity by zone and by system.
- Freeze critical interface dimensions before issuing fabrication packages.
- Separate provisional drawings from approved production documents.
- Track revision impact on bought-out items and custom fabrications.
- Confirm access routes and maintenance envelopes, not only nominal coordinates.
In practical terms, shipbuilding equipment for outfitting should be released in batches that reflect construction logic.
That means design teams, outfit planners, and suppliers work from the same zone priorities.
Otherwise, early deliveries can still become late installations.
Supplier Coordination Often Decides Delivery Reliability
Not all delays come from manufacturing capacity.
A large share comes from weak coordination across drawing approval, material confirmation, inspection timing, and shipping readiness.
For shipbuilding equipment for outfitting, this matters because many items are interdependent.
A delayed support frame can hold up piping.
A missing penetration piece can stall cable pulling.
A vendor package without final tagging can create identification errors onboard.
The stronger approach is to manage suppliers through interface checkpoints, not only promised dates.
What Should Be Checked Early
- Bill of materials completeness and approved substitutions.
- Fabrication drawing alignment with latest yard standards.
- Marking, tagging, and packing lists matched to installation zones.
- Inspection hold points tied to actual production milestones.
- Export packing requirements for moisture, corrosion, and shock protection.
This also means commercial follow-up should connect with engineering status.
A supplier that looks on schedule on paper may still be exposed to revision churn or unresolved technical queries.
That gap is where many shipbuilding equipment for outfitting delays begin.
Fabrication Tolerance Has a Direct Effect on Fit-Up Quality
Fit-up quality depends on more than whether an item arrives at the yard.
It depends on whether it matches the installation condition without forced adjustment.
For shipbuilding equipment for outfitting, small dimensional errors can turn into major onboard work.
Misaligned holes, distorted frames, poor weld shrinkage control, and inconsistent bracket positioning are recurring causes.
These problems are expensive because they consume labor during congested installation windows.
More importantly, they can affect downstream painting, insulation, commissioning, and class inspection.
High-Risk Tolerance Points
- Foundation bolt patterns and leveling surfaces.
- Modular pipe spool interfaces and flange orientation.
- Support elevations across multi-discipline routing corridors.
- Door, panel, and hatch clearances in confined spaces.
- Skid lifting points that affect transport and final placement.
When reviewing shipbuilding equipment for outfitting, dimensional inspection should focus on installation-critical features.
Checking only general length and width is rarely enough.
The more useful question is whether the item can be installed as planned, with approved tolerances and no field redesign.
Logistics and Packaging Can Undermine Good Manufacturing
Even well-made shipbuilding equipment for outfitting can arrive in poor condition.
Heavy handling, sea transport, storage exposure, and mixed-package delivery often create hidden damage.
Bent supports, lost fasteners, chipped coatings, and moisture intrusion all affect final fit-up quality.
This becomes more serious when installation windows are short.
There may be no time for repair or replacement.
In actual projects, the best results come from packaging that follows installation logic.
Zone-based packing, clear labels, and protected critical surfaces save time long after unloading.
For global trade participants, this is also where import timing and port handling matter.
A delayed customs release can be just as disruptive as a late fabrication finish.
Installation Sequencing Is Where Delivery and Quality Finally Meet
Shipbuilding equipment for outfitting is rarely installed in isolation.
It must fit the block erection plan, hot work restrictions, coating status, and access availability.
This means a technically correct item can still become a schedule problem if delivered in the wrong sequence.
A practical installation strategy usually answers three questions early.
- Can the equipment be installed before space becomes congested?
- Will later trades damage or obstruct the installed item?
- Are testing and commissioning needs built into the sequence?
This is why pre-outfitting and modularization continue to gain attention.
When suitable shipbuilding equipment for outfitting is assembled earlier, yards often improve access, safety, and dimensional control.
Still, modular work only helps when dimensions, lifting plans, and interface checks are reliable.
Otherwise, problems simply move upstream.
How to Improve Shipbuilding Equipment for Outfitting Performance
The most effective improvements are usually operational, not theoretical.
They connect engineering, supply chain, fabrication, and yard execution into one decision flow.
For shipbuilding equipment for outfitting, the following actions tend to produce the fastest results.
- Use zone-based release planning instead of bulk purchase release.
- Create interface registers for each critical outfitting package.
- Link supplier progress reviews to technical closure status.
- Inspect installation-critical dimensions before shipment.
- Align packing, labeling, and delivery sequence with yard work fronts.
- Capture fit-up deviations and feed them back into future sourcing decisions.
This also supports better market decisions.
As industrial supply chains shift, buyers need more than price visibility.
They need timely insight into supplier reliability, trade exposure, compliance changes, and manufacturing readiness.
That broader view helps teams protect both schedule and fit-up quality.
Conclusion
Reliable shipbuilding equipment for outfitting comes from disciplined control across the full project chain.
Design maturity, supplier coordination, tolerance control, logistics, and installation sequencing all shape the final result.
When these elements are managed together, delivery improves and fit-up quality becomes more predictable.
The next practical step is to review current outfitting packages by interface risk, not only by promised delivery date.
That shift usually reveals where schedule pressure and onboard rework are really coming from.