Related News
 What to Check Before Sourcing a YLCSD350 Cutter Suction Dredger for ProjectsAug 24, 2026
 Battery Cage System of Poultry Farming: What Determines Layer CapacityAug 21, 2026
- China’s Lithium Battery Chain Sees Strong Q2; Overseas Storage Orders LandAug 16, 2026
- China Expands Cross-Border Cash Pooling for Multinationals NationwideAug 15, 2026
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.
Manufacturing Plant Layout Design: Layout Mistakes That Slow Production





In manufacturing, even small layout flaws can create major bottlenecks, raising handling costs, extending cycle times, and reducing overall equipment efficiency. For project managers and engineering leaders, effective manufacturing plant layout design is not just about space planning—it directly shapes productivity, safety, and scalability. This article examines the most common layout mistakes that slow production and how to avoid them.
What makes this issue especially important is that layout risk does not look the same in every operating environment. A greenfield heavy-equipment plant, a metals processing workshop, a packaging line expansion, and a retrofit inside an old industrial building all face different constraints. The same manufacturing plant layout design choice may improve flow in one setting and create chronic delays in another. For project managers and engineering leads, the real task is not simply choosing a “good layout,” but identifying which layout decisions fit the production scenario, material profile, labor model, utility demand, and future growth path.
Why layout mistakes vary by production scenario
In industrial operations, layout errors usually emerge where planning assumptions do not match reality. A plant handling bulky fabricated components needs wider transport corridors and larger staging zones than a facility assembling compact parts. A continuous process line depends on uninterrupted equipment sequence, while a job-shop environment requires routing flexibility. This is why manufacturing plant layout design should always be assessed through the lens of application scenario rather than through generic checklists alone.
For project teams in the broader industrial value chain, layout affects more than production speed. It influences maintenance access, forklift traffic, environmental compliance, worker safety, export packing efficiency, expansion feasibility, and even energy use. In heavy industry and related sectors, poor physical arrangement can quickly turn into higher operating cost, delayed order fulfillment, and reduced competitiveness.
Typical scenarios where manufacturing plant layout design often fails
1. Greenfield plants that prioritize construction convenience over material flow
In new plant projects, teams sometimes lock building structure, office placement, and utility routing too early, before validating product flow. The result is a plant that looks orderly on paper but forces materials to zigzag between receiving, machining, assembly, inspection, and shipping. In this scenario, the main layout mistake is treating architecture as fixed and production logic as adjustable. For project leaders, manufacturing plant layout design should begin with flow maps, takt assumptions, and handling paths before finalizing building details.
2. Brownfield retrofits constrained by legacy buildings
Older factories often inherit column grids, low clear heights, outdated utility lines, and fragmented work areas. A common error is forcing new equipment into leftover spaces without redesigning supporting flows. This creates hidden bottlenecks around loading points, maintenance zones, and intermediate buffers. In retrofit scenarios, manufacturing plant layout design must account for what cannot be changed and focus on what can be re-sequenced, combined, or relocated to reduce backtracking.
3. High-mix, low-volume operations using a line layout that is too rigid
Plants producing customized industrial products often struggle when management copies a straight-line layout from mass production environments. If routing changes by product type, a rigid line can create idle stations, repeated handling, and scheduling conflicts. In this application scenario, the problem is not insufficient structure but insufficient flexibility. A cellular or modular arrangement may outperform a fixed sequence line.
4. Bulk-material or heavy-component sites with underestimated movement needs
In steel, mining support equipment, petrochemical modules, and construction machinery manufacturing, material size and weight strongly shape the layout. Teams often underestimate crane coverage, turning radius, floor loading, and temporary staging demand. That misjudgment slows production because large items cannot move when needed, forcing rescheduling and unsafe workarounds. Here, manufacturing plant layout design must be built around actual handling constraints, not only equipment footprints.
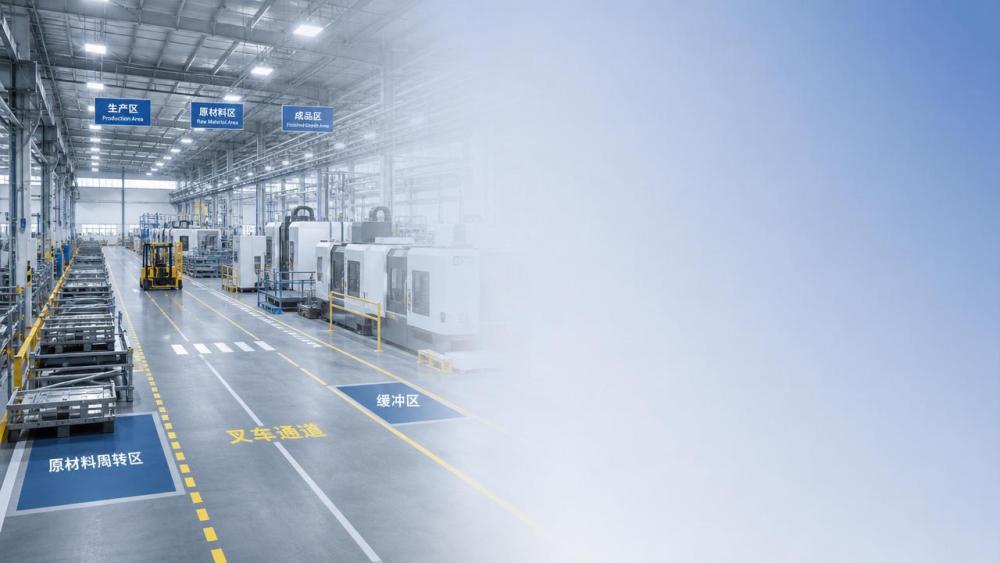
A scenario comparison: where the priorities change
The table below helps project managers evaluate how layout priorities shift across common industrial production environments. This comparison is useful when deciding whether a current manufacturing plant layout design approach is suitable or likely to introduce delays.
The layout mistakes that most often slow production
Poor relationship between receiving, storage, and first process
One of the most frequent manufacturing plant layout design failures is placing raw material storage far from the first value-adding step. This issue is common in plants that expanded gradually or repurposed available floor area. Every additional movement adds labor, equipment usage, waiting time, and congestion. In heavy industry, where material units are larger and handling costs are higher, this mistake can significantly reduce throughput. Project teams should evaluate whether inbound flow supports direct, short, and predictable transfer into production.
Ignoring internal logistics intensity
Many layouts are drawn around machines rather than around movement frequency. But a station touched dozens of times per shift should not be treated the same as a rarely used area. When planners overlook tugger routes, forklift intersections, returnable packaging loops, or waste removal paths, transport conflicts become unavoidable. This is especially damaging in facilities with both pedestrian activity and powered material handling. A practical manufacturing plant layout design review should quantify trips per hour, route overlap, queue points, and crossing risks.
Insufficient buffer strategy between unstable processes
Buffers are often misunderstood. Some plants have too little intermediate storage, causing one disruption to stop the entire line. Others have too much poorly located inventory, which hides process problems and consumes space needed for movement. The right answer depends on the production scenario. A continuous line with stable cycle times may need minimal buffers, while a fabrication-and-assembly environment with variable process duration needs controlled decoupling points. Good manufacturing plant layout design uses buffers strategically, not accidentally.
Maintenance access treated as a secondary issue
A layout can look efficient during startup yet become costly during operations if technicians cannot safely access critical systems. Equipment packed too tightly may reduce floor use on paper, but it raises downtime when repairs, cleaning, calibration, or parts replacement are needed. For project managers, this is a classic scenario of short-term fit versus long-term operability. In manufacturing plant layout design, maintenance paths, isolation zones, lifting access, and spare-parts service points should be planned from the beginning.
No room for product mix shifts or future expansion
Industrial markets change. New export requirements, customer specifications, automation upgrades, environmental controls, or energy systems can alter layout needs faster than expected. Yet many plants are arranged to maximize immediate occupancy rather than future adaptability. This is risky in sectors exposed to policy updates, trade shifts, or technology upgrading. Effective manufacturing plant layout design should reserve logical expansion corridors, utility capacity, and relocation options for critical operations.
How layout priorities differ by stakeholder and business need
Different decision-makers often evaluate the same plant from different angles. Misalignment among stakeholders is itself a source of layout error. The best manufacturing plant layout design process makes those priorities visible early.
Scenario-based recommendations for better manufacturing plant layout design
If your plant is launching a new line
Build the layout from process sequence and logistics demand, not from building symmetry. Simulate material movement before construction finalization. Test operator travel, replenishment frequency, and maintenance access under realistic production loads.
If your site is upgrading inside a constrained facility
Identify the true bottleneck interfaces first: inbound staging, first process entry, shared utilities, aisle conflict points, and shipping exits. In retrofit conditions, improving one interface may produce more throughput gain than moving many machines.
If your operation handles heavy or oversized items
Plan around movement envelopes, not nominal dimensions. Confirm crane hook paths, floor loading, turning radii, and temporary set-down needs. Seemingly small underestimates in these areas can have major effects on production continuity.
If your product mix changes often
Choose modular work zones, flexible utilities, and shared resources that support rerouting without full redesign. In this scenario, the best manufacturing plant layout design is often the one that preserves flow while allowing controlled variation.
Common misjudgments project teams should avoid
A frequent misjudgment is assuming that high space utilization means high efficiency. In reality, an overcrowded plant often has lower productivity because circulation, visibility, maintenance, and safety all deteriorate. Another mistake is relying on static equipment layouts without validating shift-level logistics behavior. Teams also tend to underestimate non-production spaces such as inspection, rework, packaging, scrap handling, and tool storage, even though these functions strongly influence real flow. Finally, many projects design for day-one demand only, despite the fact that industrial businesses must respond to policy changes, decarbonization requirements, export market shifts, and automation upgrades.
FAQ: practical questions about manufacturing plant layout design
How can a project manager tell if a layout is slowing production?
Look for repeated handling, long travel distances, queue buildup between processes, blocked aisles, and unplanned work-in-process storage. If schedule pressure is constant despite adequate equipment capacity, the manufacturing plant layout design may be part of the problem.
Is a straight production line always best?
No. It works well in stable, repetitive environments, but can perform poorly in high-mix or space-constrained operations. The best layout depends on product routing, variability, handling method, and expansion plans.
When should a company redesign instead of making minor layout fixes?
A broader redesign is usually justified when bottlenecks are systemic, safety conflicts are recurring, major automation is planned, or product and volume profiles have changed significantly from the original plant assumptions.
Final takeaways for project and engineering leaders
Strong manufacturing plant layout design is not about copying a standard arrangement. It is about matching flow, equipment, safety, and growth needs to the actual production scenario. For project managers and engineering leaders, the most effective approach is to evaluate layouts through real operating conditions: what moves, how often, in what sequence, under what constraints, and with what future changes in mind. If your plant is preparing a new build, an expansion, or a retrofit, start by defining the scenario clearly, comparing layout options against that scenario, and validating decisions with cross-functional stakeholders before costly bottlenecks are built into the facility.