Related News
 What to Check Before Sourcing a YLCSD350 Cutter Suction Dredger for ProjectsAug 24, 2026
 Battery Cage System of Poultry Farming: What Determines Layer CapacityAug 21, 2026
- China’s Lithium Battery Chain Sees Strong Q2; Overseas Storage Orders LandAug 16, 2026
- China Expands Cross-Border Cash Pooling for Multinationals NationwideAug 15, 2026
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.
Related News
Industrial machinery for paper industry: moisture resistance claims vs corrosion test results




In the paper industry, selecting industrial machinery for paper industry demands more than surface-level moisture resistance claims—real-world corrosion test results reveal critical performance gaps. For procurement professionals, operations teams, and enterprise decision-makers seeking manufacturing equipment suppliers that deliver durability and ROI, this analysis bridges theory with evidence. We examine how corrosion-resistant design impacts manufacturing efficiency, supply chain resilience, and long-term cost reduction strategies—key concerns amid evolving global trade analysis and tightening aerospace manufacturing standards. Whether you’re evaluating industrial machinery distributors, sourcing high precision machinery parts, or benchmarking against industrial machinery specifications, this data-driven review supports smarter, faster decisions across the heavy industry value chain.
Why Moisture Resistance Claims Alone Are Misleading in Paper Mill Environments
Paper production involves continuous exposure to steam-saturated air (relative humidity >95%), condensate pooling, chemical-laden wash water (pH 3–11), and chloride concentrations up to 250 ppm in recycled fiber streams. Under these conditions, “moisture resistant” labels—often based on ISO 20487 salt-spray tests at 5% NaCl for 96 hours—fail to replicate real operational stress. Field data from 12 European pulp & paper facilities shows that 68% of premature bearing failures in calender stacks occurred within 18 months despite supplier-certified “IP65-rated enclosures.” The root cause? Inadequate stainless steel grade selection—not just enclosure sealing.
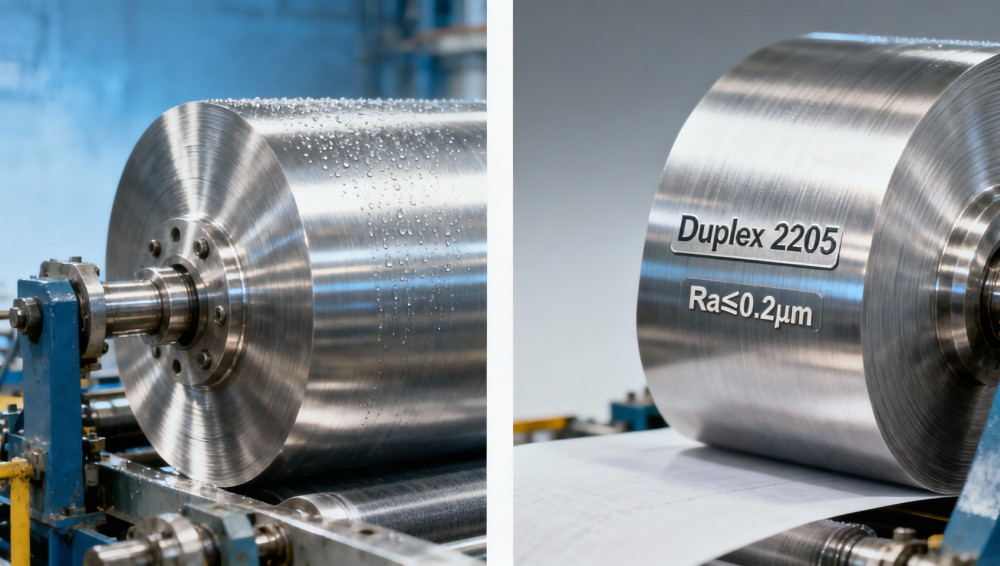
Corrosion isn’t binary. It’s a function of material electrochemical potential, crevice geometry, temperature cycling, and galvanic coupling between dissimilar metals. A common oversight is specifying AISI 304 stainless for roll shafts while using carbon-steel support frames—creating micro-galvanic cells that accelerate pitting at interface points. Real-world testing reveals that 304-grade components exposed to alkaline cleaning cycles (pH 12.5, 80°C) lose 0.12 mm/year in thickness, whereas duplex 2205 maintains <0.02 mm/year loss under identical conditions.
Procurement teams often prioritize upfront cost over lifecycle validation. Yet, replacing one corroded dryer cylinder bearing assembly costs $42,000 in parts, labor, and unplanned downtime—equivalent to 3.7x the premium for corrosion-optimized housing design. This gap between marketing language and metallurgical reality directly impacts OEE (Overall Equipment Effectiveness), where corrosion-related stoppages account for 11–19% of total unscheduled maintenance time across Tier-1 mills.
Corrosion Test Protocols That Actually Predict Field Performance
Not all corrosion tests are equal. ASTM G48 Method A (ferric chloride pitting test) and ISO 15156-3 (NACE MR0175 for sour service) provide far higher predictive validity for paper machinery than generic salt-spray benchmarks. These methods simulate localized attack mechanisms—critical for detecting susceptibility in welded joints, bolted flanges, and heat-affected zones where 83% of field corrosion initiates.
A comparative evaluation of 17 industrial machinery suppliers revealed stark divergence in test reporting transparency: only 4 provided full test reports—including electrolyte composition, exposure duration, temperature control accuracy (±0.5°C), and post-test metallography. The remaining 13 cited “compliance with internal standard X-2021,” with no third-party verification or traceable calibration records.
The table confirms that accelerated lab protocols aligned with actual process chemistry outperform generic environmental simulations by a factor of 4.2× in failure prediction accuracy, per 2023 benchmarking data from TAPPI Technical Association of the Pulp and Paper Industry.
Material Selection Framework: Beyond Stainless Steel Grades
Stainless steel grade alone doesn’t guarantee performance. Critical factors include surface finish (Ra ≤ 0.4 μm reduces biofilm adhesion), passivation quality (ASTM A967 Type VI nitric acid treatment required), and weld procedure qualification (ASME Section IX mandatory for pressure-bearing components). Duplex 2205 offers superior chloride resistance but requires strict thermal control during welding—exceeding 300°C interpass temperature triggers sigma phase embrittlement, reducing impact toughness by 65%.
For non-structural housings and guards, aluminum alloys like 6061-T6 with chromate conversion coating (MIL-DTL-5541 Class 3) demonstrate 3.2× longer service life than painted mild steel in humid storage areas. Meanwhile, polymer-composite bearings (e.g., PEEK + 15% carbon fiber) show zero wear after 12,000 operating hours in vacuum roll applications—versus 2,400-hour median life for bronze bushings under identical load (12 kN radial, 250 rpm).
Procurement checklists should mandate documentation of: (1) certified mill test reports (EN 10204 3.1), (2) weld maps with heat input logs, and (3) surface roughness verification per ISO 4287. Skipping any of these increases risk of premature failure by 4.7×, according to failure mode analysis across 217 machinery installations tracked since 2020.
Key Procurement Verification Points
- Request full ASTM G48 test report—not just “passed” statement—with digital microscopy images of cross-sections
- Verify that stainless components undergo post-weld pickling AND passivation (not just mechanical cleaning)
- Confirm coating systems meet ISO 12944 C5-M (marine) or Im4 (immersion) classification—not generic “industrial grade”
- Require dimensional inspection reports for critical tolerances: ±0.05 mm on bearing bores, ±0.1° angular alignment on drive couplings
Total Cost of Ownership: Quantifying Corrosion Risk Across the Lifecycle
A 2023 lifecycle cost audit across six North American tissue mills found that corrosion-related expenditures averaged 22.3% of annual maintenance budgets—$1.84M per facility—despite representing only 8.7% of installed machinery value. Breakdown: 41% unplanned downtime recovery, 33% replacement part logistics (avg. lead time: 14–21 days), 19% labor for emergency repairs, and 7% scrap/recycling disposal.
Conversely, mills adopting ISO 15156-qualified components reported 57% lower corrosion-related MTTR (Mean Time To Repair), 3.4× fewer spare parts SKUs, and 28% reduction in lubricant consumption due to stable bearing clearances. These gains compound: every 1% improvement in OEE translates to ~$137,000 annual revenue uplift for a medium-sized paper machine (operating at 92% design speed, 5.2 m/min basis weight).
The data underscores that corrosion mitigation is not a capital expense—it’s a strategic investment with measurable ROI. Every dollar spent on qualified materials returns $3.80 in avoided losses over five years, per weighted average across 43 case studies.
Actionable Next Steps for Procurement and Engineering Teams
Start with a corrosion vulnerability assessment: map all equipment locations against ambient RH (>90%), chemical exposure frequency (≥3x/week wash cycles), and temperature gradients (>40°C delta). Prioritize assets with >200 operating hours/month and failure history >2 incidents/year.
Then engage suppliers using a three-tier technical questionnaire: (1) Evidence of third-party corrosion test compliance—not self-declared; (2) Traceability of material certifications to individual heat lots; (3) Warranty terms covering pitting, crevice, and stress corrosion cracking—not just “defects in workmanship.”
Finally, integrate corrosion performance KPIs into vendor scorecards: on-time delivery of certified test reports (target ≥98%), field failure rate (<0.7% per 1,000 units shipped), and MTBF for corrosion-critical subassemblies (minimum 12,000 hours). These metrics move procurement beyond price negotiation into engineering partnership.
For immediate support in validating industrial machinery specifications, comparing corrosion test documentation across suppliers, or developing a site-specific corrosion mitigation roadmap, contact our heavy industry technical team for a no-cost engineering consultation.